Premium Gym Bag Manufacturer for Global Brands
Turn your concepts into reality. As a specialized athletic bag factory, we offer end-to-end custom manufacturing—from design to global delivery.
Premium Gym & Fitness Duffel Collection
Explore our versatile range of sports bags, from lightweight drawstring backpacks to heavy-duty training duffels. Built for maximum durability and style. By partnering directly with an experienced gym bag manufacturer, you gain access to factory-direct wholesale prices, low MOQs, and expert guidance to build your fitness brand.
custom backpack
custom chest bag
custom crossbody bag
Custom messenger bag
custom Duffel bag
custom waterproof bag
custom travel bag
custom tactical bag
- Tactical Sling & EDC Bags
- Tactical Duffle & Deployment Bags
- Pistol Range & Shooting Gear Bags
- Rifle Cases & Drag Bags
- Tactical Backpacks & Go Bags
- Tactical Messenger & Laptop Bags
- Tactical Diaper Bags for Dads
- Medical & First Responder Bag
- Chest Rigs & Waist Packs
- Tactical Lunch & Cooler Bags
- Police & Law Enforcement Gear
- Tactical Accessories & Pouches
Custom Hiking bag
Custom fishing bag
custom surfboard bag
Custom bike bag
custom tool bag
custom cooler bag
Custom Lunch bag
Custom mackup bag
custom hunting bag
custom gym bag
custom ski bag
custom pet carrier
custom diaper bag
- Ergonomic Diaper Backpacks
- Tactical Diaper Bag Series
- Vegan Leather Baby Bags
- Travel & Overnight Diaper Bags
- Sustainable (GRS) Diaper Bags
- Gender-Neutral Parenting Packs
- Fashion Diaper Totes for Women
- 3-in-1 Convertible Diaper Bags
- Universal Stroller & Pram Organizers
- Messenger & Satchel Changing Bags
- Water-resistant Nylon Baby Bags
- Portable Diaper Changing Clutches
Get Sample
See the quality before you buy

Gym Duffle Bag

Drawstring Gym Bag

Waterproof Gym Bag

Tactical Gym Bag

Gym Bag Backpack

Gym Bag With Shoe Compartment

Gym Bag With Yoga Mat Holder

Leather Gym Bag

Gym Tote Bag

Gym Bag With Laptop Compartment

Boxing Gym Bag

Small Gym Bag
Premium High-Performance Fabrics for Custom Gym Bags
As a trusted gym bag manufacturer, we know material quality drives your brand’s premium. We utilize high-performance fabrics—including tear-resistant Ripstop Nylon, waterproof TPU coatings, and eco-friendly rPET. Our custom OEM/ODM solutions guarantee lightweight durability, a stable supply chain, and competitive wholesale value. Elevate your product line with textiles engineered for rigorous training.

What is 600D/900D Polyester?
600D/900D Polyester is a heavy-duty, plain-weave synthetic fabric. It is the global industry standard for entry-level to mid-range athletic gear. If you are manufacturing a durable gym bag, this material offers the ultimate balance of tensile strength, affordability, and high-volume scalability.
Why source this for your production?
- Unbeatable Cost-Performance: Delivers high tear resistance at a fraction of nylon’s cost. Perfect for maximizing margins on promotional or wholesale gym bags.
- High Workability: Its inherent stiffness ensures smooth cutting and sewing. This significantly reduces defect rates and material waste on the assembly line.
- Easy Customization: The smooth oxford surface is highly receptive to screen printing and heat transfer—ideal for branded custom gym bags.
- Proven Market Acceptance: Consumers universally trust the classic “oxford” texture for reliable, daily-use sports gear.
Key supply parameters:
- Weight (GSM): 200 – 350 g/m² (varies by yarn density and coating).
- Width: Standard 58″/60″ (147cm – 152cm) to maximize cutting yield.
- Coating: Available in PU for a lightweight waterproof gym bag, or PVC for maximum stiffness and lowest cost.
- Compliance: Engineered to meet REACH, RoHS, and OEKO-TEX Standard 100. GRS-certified recycled (rPET) options available.
Sourcing Tip: To avoid high custom-dye MOQs, use standard stock colors (Black, Navy, Heather Grey) for the main body and contrast webbing for branding. For EU/US exports, always specify “REACH-compliant PU” or “Phthalate-free PVC” to prevent customs issues.

What is High-Density / Ripstop Nylon?
High-Density Ripstop Nylon is a premium, plain-weave synthetic fabric featuring a signature reinforced crosshatch grid. Positioned for the mid-to-high-end market, it is the ultimate material for crafting a high quality gym bag. It delivers exceptional tear resistance and a modern, parachute-like aesthetic, allowing brands to command higher retail margins.
Why source this for your production?
- Premium Market Appeal: Consumers instantly recognize the ripstop grid as high-end technical gear. Perfect for launching a premium, lightweight gym bag collection.
- High Workability: The reinforced grid ensures dimensional stability. This prevents fraying during automated cutting and ensures smooth sewing for any complex gym duffel bag.
- Advanced Finishing: Highly compatible with PU backings and DWR treatments. It provides weatherproofing while remaining soft enough to fold into a compact gym bag.
Key supply parameters:
- Weight (GSM): 40 – 120 g/m² (typically 70D to 210D).
- Width: Standard 58″/60″ (147cm – 152cm) to maximize cutting yield.
- Coating: Light PU clear coat (internal) paired with a DWR face finish (external).
- Compliance: REACH, RoHS, and OEKO-TEX Standard 100. GRS-certified Recycled Nylon (rNylon) available.
Sourcing Tip: When manufacturing a nylon gym bag, avoid thick PU backings that make the fabric stiff and cheap. Request a “light PU kiss coat” to maintain a soft drape while passing water-resistance tests. Note: Nylon requires specialized acid dyeing, so expect slightly higher MOQs for custom Pantone colors compared to polyester.

What is Neoprene?
Neoprene (polychloroprene) is a premium synthetic rubber foam core, double-laminated with fine-gauge polyester or nylon jersey. Positioned in the mid-to-premium market, its inherent cushioning and structured drape instantly elevate perceived product value. It is the ultimate material for crafting a stylish gym bag, allowing brands to command higher retail margins in the boutique fitness sector.
Why source this for your production?
- Premium Market Demand: Consumers associate neoprene’s smooth, spongy texture with high-end athleisure. It is highly sought-after for trendy womens gym bags that transition seamlessly from the studio to the street.
- Streamlined Workability: The thick foam core eliminates the need for extra stiffeners or EVA foams. This drastically reduces assembly time and labor costs when manufacturing a structured gym tote bag.
- Versatile Finishing: The outer jersey layer acts as a flawless substrate. It is highly receptive to vibrant sublimation printing and 3D embossing, perfect for visually differentiating a gym and yoga bag.
Key supply parameters:
- Thickness: 2.0mm – 3.0mm foam core (optimal for luggage).
- Width: Standard sheets of 51″ x 130″ (130cm x 330cm) or continuous 54″ rolls.
- Lamination: Double-sided (Polyester for cost-efficiency; Nylon for a softer hand-feel).
- Compliance: REACH, RoHS, and OEKO-TEX Standard 100. Eco-friendly limestone neoprene is available.
Sourcing Tip: When manufacturing a neoprene gym bag, distinguish between CR (100% Chloroprene) and SBR (Styrene Butadiene). Pure CR is for wetsuits and overkill for bags. A 30% CR / 70% SBR blend offers the perfect cost-to-performance ratio. Always explicitly specify “low-odor lamination glue” in your PO to prevent off-gassing complaints during unboxing.

What is TPU Coated Tarpaulin?
TPU (Thermoplastic Polyurethane) Coated Tarpaulin is a premium composite fabric featuring a high-tenacity polyester filament base sealed with an advanced TPU layer. Positioned in the premium market, it is the eco-friendly, modern successor to PVC tarp. Its core commercial value is expedition-grade weatherproofing and extreme abrasion resistance—the ultimate material for manufacturing a high-margin tactical gym bag or a rugged heavy duty gym bag.
Why source this for your production?
- Premium Market Demand: The matte, technical aesthetic of TPU appeals directly to consumers wanting “over-engineered” gear. It is highly sought-after for crafting a premium crossfit gym bag or a tough mma gym bag.
- Advanced Workability: TPU is highly receptive to High-Frequency (HF) and ultrasonic welding. This allows factories to create seamless, leak-proof interiors with zero needle holes—perfect for designing a gym bag with wet compartment.
- Eco-Conscious Compliance: Inherently free from toxic plasticizers and PVC. TPU ensures your products pass the strictest EU and North American customs inspections without delays.
Key supply parameters:
- Weight (GSM): 400 – 600 GSM (Balances structural integrity with daily carry weight).
- Width: 58″/60″ (147cm – 152cm).
- Coating: Single or double-sided TPU lamination (Matte or subtle gloss finish).
- Compliance: REACH, RoHS, and OEKO-TEX Standard 100 (100% Phthalate-free).
Sourcing Tip: Always explicitly specify Polyether-based TPU (not Polyester-based) on your PO. Polyether TPU offers superior hydrolysis resistance, preventing the coating from peeling or becoming sticky when exposed to sweat and damp towels. Also, note that custom Pantone colors require higher MOQs (1,000+ yards) than PVC; utilize stock colors like Tactical Black for initial market testing.

What is rPET / Recycled Polyester?
rPET (Recycled Polyethylene Terephthalate) is a sustainable textile engineered by extruding post-consumer plastic bottles into high-strength continuous filament yarns. Typically woven in 300D to 600D Plain or Ripstop structures, it sits firmly in the mid-range to premium market. Its core commercial value is instantly elevating brand equity—allowing you to market a highly profitable sustainable gym bag to today’s eco-conscious consumers.
Why source this for your production?
- Surging Market Demand: Modern buyers actively prioritize sustainable gear. Utilizing rPET provides a powerful marketing narrative, helping your products rank among the best gym bags in the premium retail space.
- Seamless Workability: rPET performs exactly like virgin polyester on the factory floor. There is zero need to adjust cutting dies or sewing machine tensions, ensuring no increase in production waste when manufacturing an everyday gym bag.
- Versatile Finishing Options: Acts as a perfect substrate for standard PU, eco-friendly TPE, or PFC-free DWR coatings. It is also highly receptive to heat transfer printing, making it ideal for a vibrant workout gym bag or a versatile travel gym bag.
Key supply parameters:
- Weight (GSM): 150 – 350 GSM (Typically 300D to 600D).
- Width: 58″/60″ (147cm – 152cm).
- Coating: PU (Polyurethane) or TPE backing for structure and weather resistance.
- Compliance: GRS (Global Recycled Standard), REACH, and OEKO-TEX Standard 100.
Sourcing Tip: Always demand a valid GRS Transaction Certificate (TC) specifically for your batch, not just a general factory audit. Without a TC, your brand cannot legally claim the material is recycled. Additionally, custom Pantone dyeing for rPET requires higher MOQs (1,000+ yards); utilize core stock colors like Black or Navy for faster turnarounds.

What is Vegan Leather / PU Leather?
Vegan Leather (Polyurethane/PU Leather) is an advanced synthetic composite featuring a high-performance PU face layer bonded to a woven filament polyester (Plain or Twill) or non-woven microfiber backing. Firmly positioned in the mid-range to premium market, it delivers the luxurious drape and hand-feel of genuine hides at a fraction of the cost—instantly elevating your product into a highly profitable luxury gym bag.
Why source this for your production?
- Exceptional Cost-Performance: Achieve the premium aesthetics and durability of a real leather gym bag at roughly 30-40% of the material cost, significantly maximizing your retail margins.
- High Workability & Yield: Supplied in uniform, continuous rolls, PU leather eliminates the irregular shapes and scars of animal hides. This guarantees seamless automated cutting, consistent sewing tension, and near-zero scrap waste.
- Surging Market Demand: Cruelty-free materials provide a compelling marketing narrative, appealing to modern consumers actively searching for an ethical yet chic gym bag.
- Versatile Finishing Options: The surface easily accepts custom embossed textures (e.g., pebble, Saffiano) and serves as a perfect substrate for debossed branding, ideal for crafting a high-end mens leather gym bag.
Key supply parameters:
- Thickness & Weight: 0.8mm – 1.2mm / 400 – 800 GSM (Engineered for structural integrity and tear resistance).
- Width: 54″/55″ (137cm – 140cm).
- Backing: Woven polyester twill or brushed non-woven microfiber.
- Compliance: REACH compliant, DMF-free (Dimethylformamide), and OEKO-TEX Standard 100.
Sourcing Tip: Always request Solvent-Free PU (Water-borne PU) for premium lines. It eliminates the harsh chemical odor upon unboxing—a major cause of negative reviews—and offers superior hydrolysis resistance (anti-peeling) against sweat and humidity. While custom grains require 500+ yards MOQ, classic pebble textures in core colors (Black, Navy, Tan) are often available in stock for rapid sampling.

What is Cordura / Ballistic Nylon?
Cordura and Ballistic Nylon are premium, highly engineered textiles woven from continuous high-tenacity nylon 6,6 filament yarns. Constructed in a dense plain weave or a heavy 2×2 basket weave, these fabrics dominate the premium to ultra-premium market tier. Their core commercial value is unparalleled abrasion and tear resistance, empowering brands to manufacture an authentic military gym bag or a rugged mens gym duffle bag that commands top-tier retail prices and supports lifetime warranties.
Why source this for your production?
- Premium Market Demand: Consumers instantly recognize and trust these materials for extreme durability. This makes it the ultimate textile choice for brands aiming to design the best work and gym bag, seamlessly transitioning from office environments to rugged training sessions.
- Heavy-Duty Workability: Despite its toughness, the fabric maintains excellent dimensional stability. It provides the necessary structural integrity and load-bearing strength required for a large gym duffle bag, cutting cleanly with minimal edge fraying when properly PU-backed.
- Advanced Finishing Options: Highly receptive to multi-pass PU (Polyurethane) back coatings for superior seam strength. It also pairs perfectly with modern C0 (PFC-free) DWR face treatments to effectively repel dirt and moisture.
Key supply parameters
- Weight (GSM): 300 – 450 GSM (Typically ranging from 500D to 1050D).
- Width: 58″/60″ (147cm – 152cm).
- Coating: 2x or 3x PU (Polyurethane) backing for enhanced rigidity.
- Compliance: REACH compliant, PFAS-free (for DWR finishes), and OEKO-TEX Standard 100 certified.
Sourcing Tip: Authentic INVISTA Cordura® requires brand registration for official marketing hangtags and carries strict MOQs (1,000+ yards). If your target retail margin is tight, ask your mill for generic “High-Tenacity Nylon 6,6.” You will achieve 90% of the physical performance at roughly 50-60% of the cost. Core tactical colors (Black, Olive Drab, Coyote Brown) typically require zero MOQ for rapid sampling.
How to prevent shoulder strap and seam failure in mass-produced gym bags?
To prevent strap and seam failure, manufacturers must utilize Bartack stitching (28-42 stitches/inch) at all stress points and high-tenacity bonded nylon thread (Tex 70+). Additionally, routing continuous load-bearing webbing around the base ensures structural integrity, even for a heavy-loaded powerlifting gym bag.

The Common Failure
Budget manufacturing relies on standard single-needle lockstitches at D-ring anchors. When consumers pack dense gear into a weightlifting gym bag or a heavy boxing gym bag, this weak stitching acts like a saw. Dynamic loading causes micro-tears, leading to catastrophic fabric blowouts and immediate 1-star reviews.
The Manufacturing Reality
True load-bearing capacity requires mechanical reinforcement and precise tension engineering:
- CNC Bartacking: We utilize programmable CNC machines to execute dense zigzag stitches directly over the webbing anchor points.
- Substrate Engineering: We pair heavy-duty stitching with PU-backed 600D-1050D fabrics. The PU coating locks the weave, preventing shifting when punctured by industrial needles (Size 18-22).
- Continuous Webbing: For hybrid designs like a gym bag backpack, we route the nylon webbing around the entire circumference. This transfers kinetic stress away from localized seams and distributes it across the continuous strap.
To guarantee zero blowouts before mass shipment, our QC engineers implement strict mechanical testing:
- Dynamic Jerk Testing (Jostle Test): Bags are loaded with 20kg (44 lbs) of steel weights and subjected to 5,000 automated drop cycles.
- Tensile Seam Strength: We use an Instron machine to pull straps directly from the fabric, strictly complying with ASTM D1683 (Standard Test Method for Failure in Sewn Seams).
- Thread Tension Calibration: Daily audits ensure optimal bobbin tension, preventing micro-abrasions on bonded threads during high-speed sewing.
Performance-Driven Solutions From Your Premier Gym Bag Manufacturer
As a dedicated gym bag manufacturer, we engineer athletic gear that meets the rigorous demands of professional fitness standards. From ventilated shoe compartments to moisture-resistant fabrics, our production capabilities ensure your inventory is gym-tested and built to withstand the toughest daily workouts.
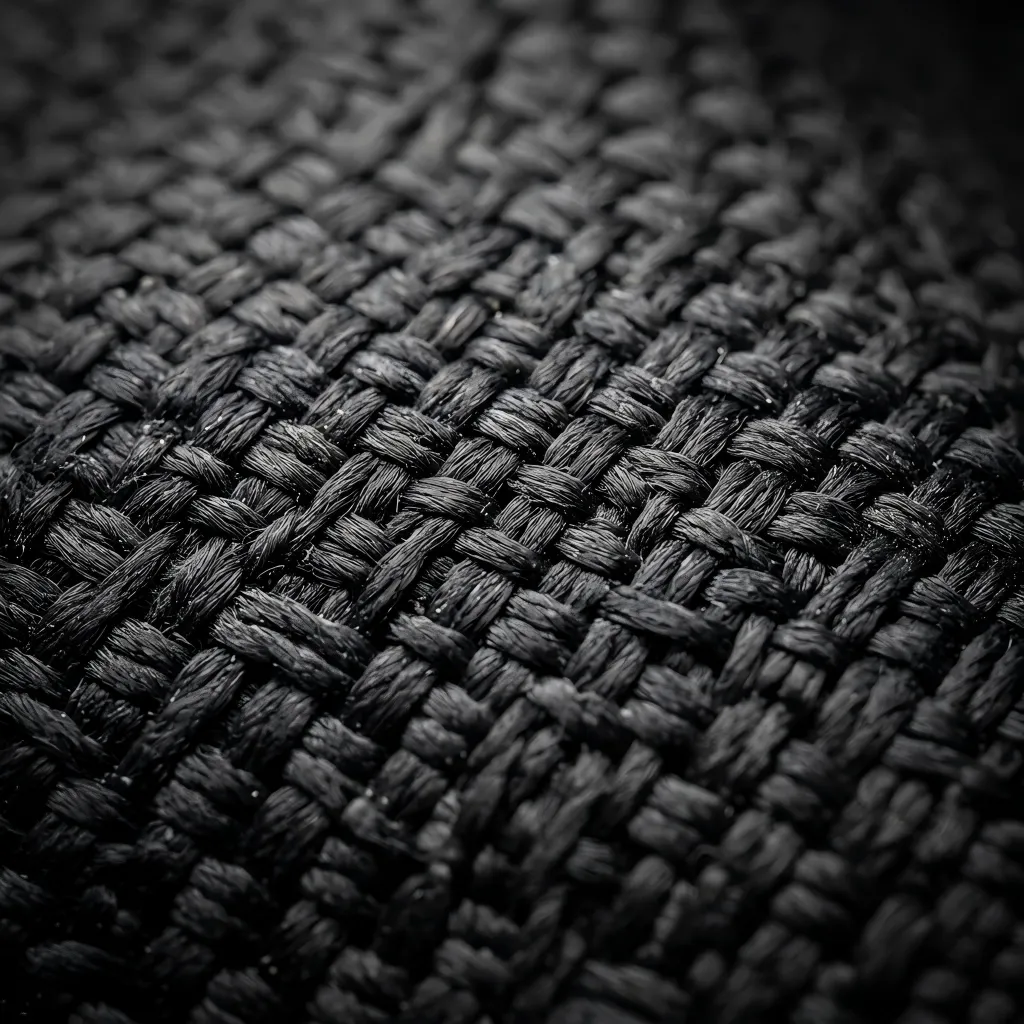
900D Ballistic Nylon Exterior
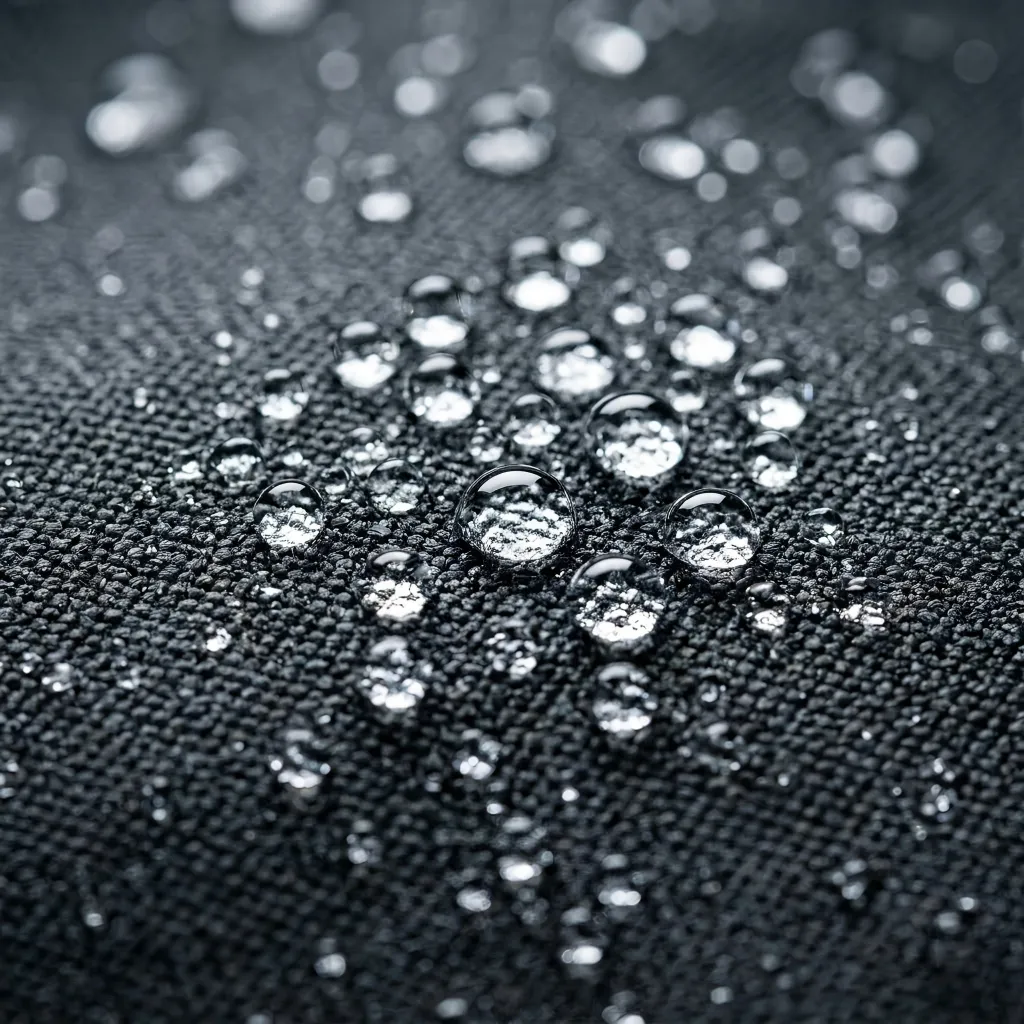
Water-Repellent DWR Face Coating
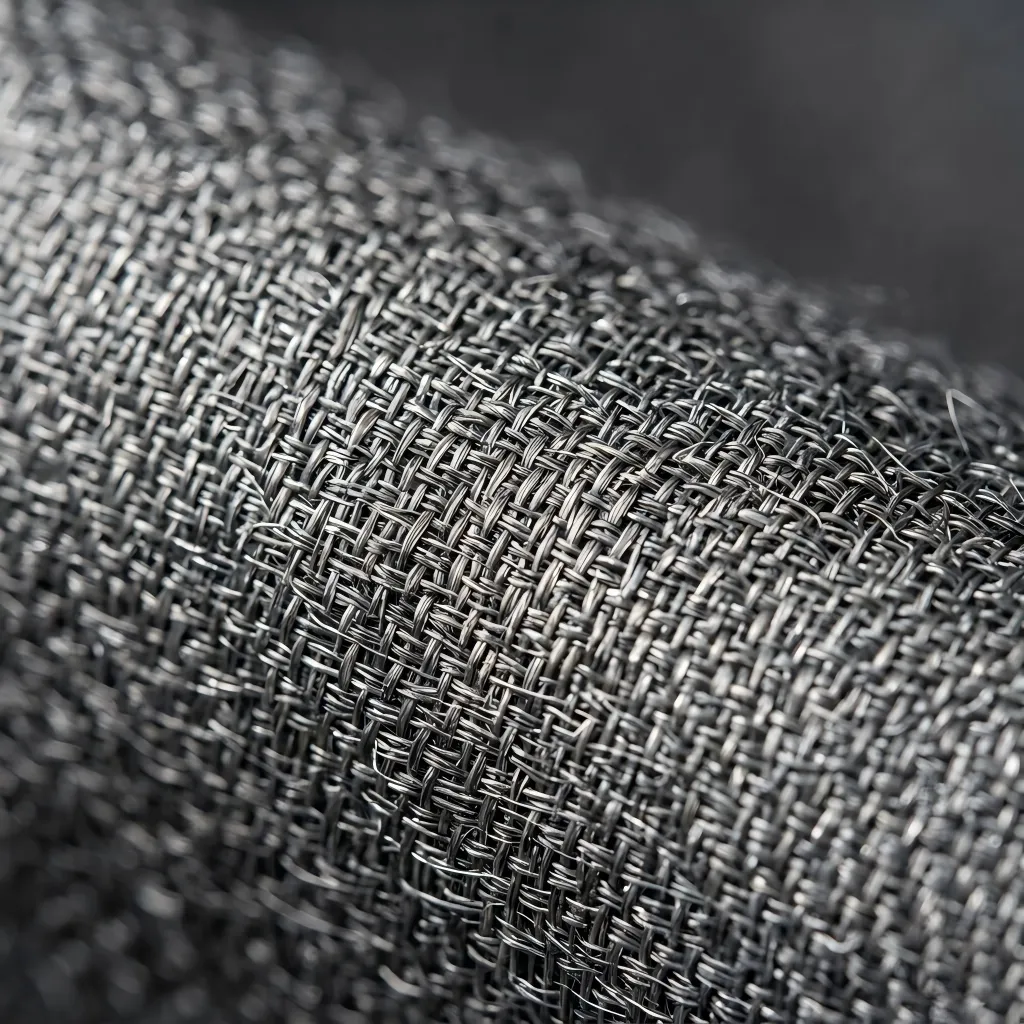
Antimicrobial Silver-Ion Lining
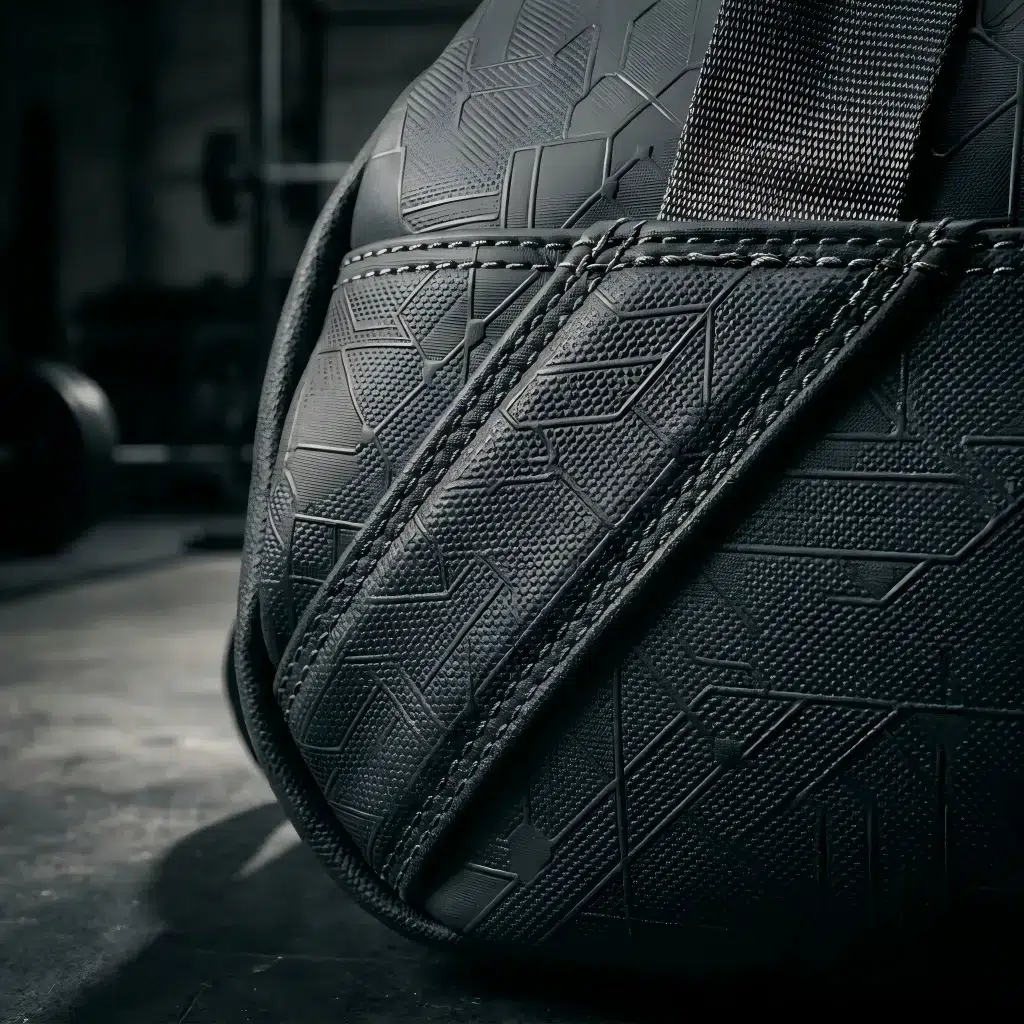
Abrasion-Resistant PU Coated Base
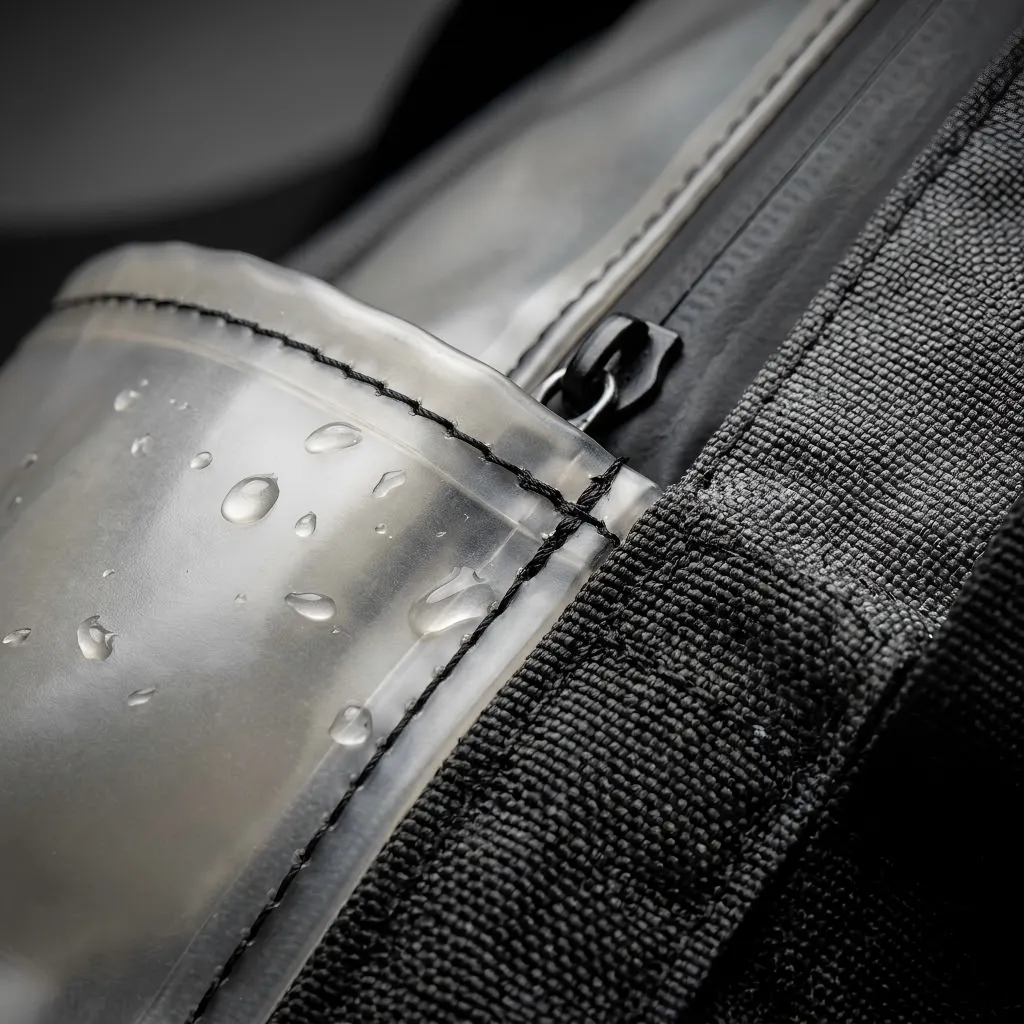
Waterproof TPU Wet Pocket
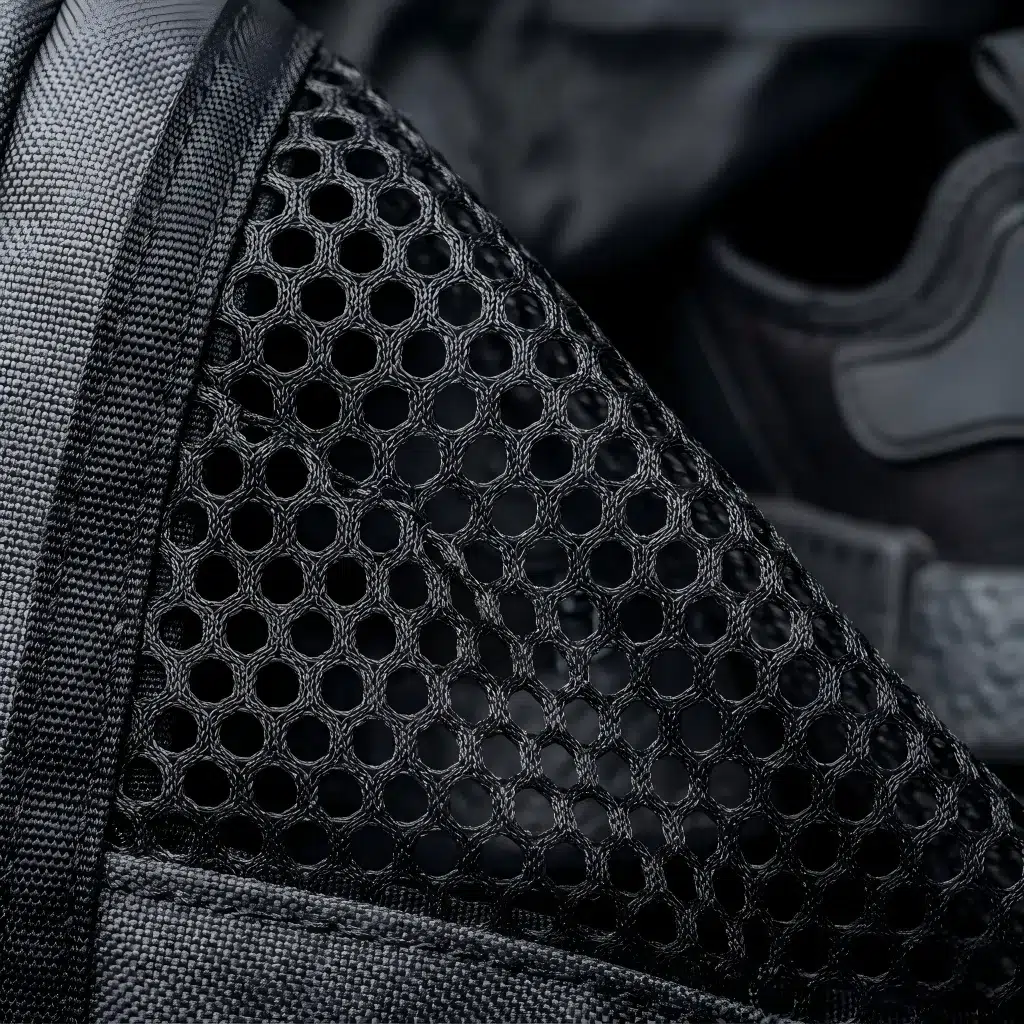
Breathable Mesh Shoe Compartment
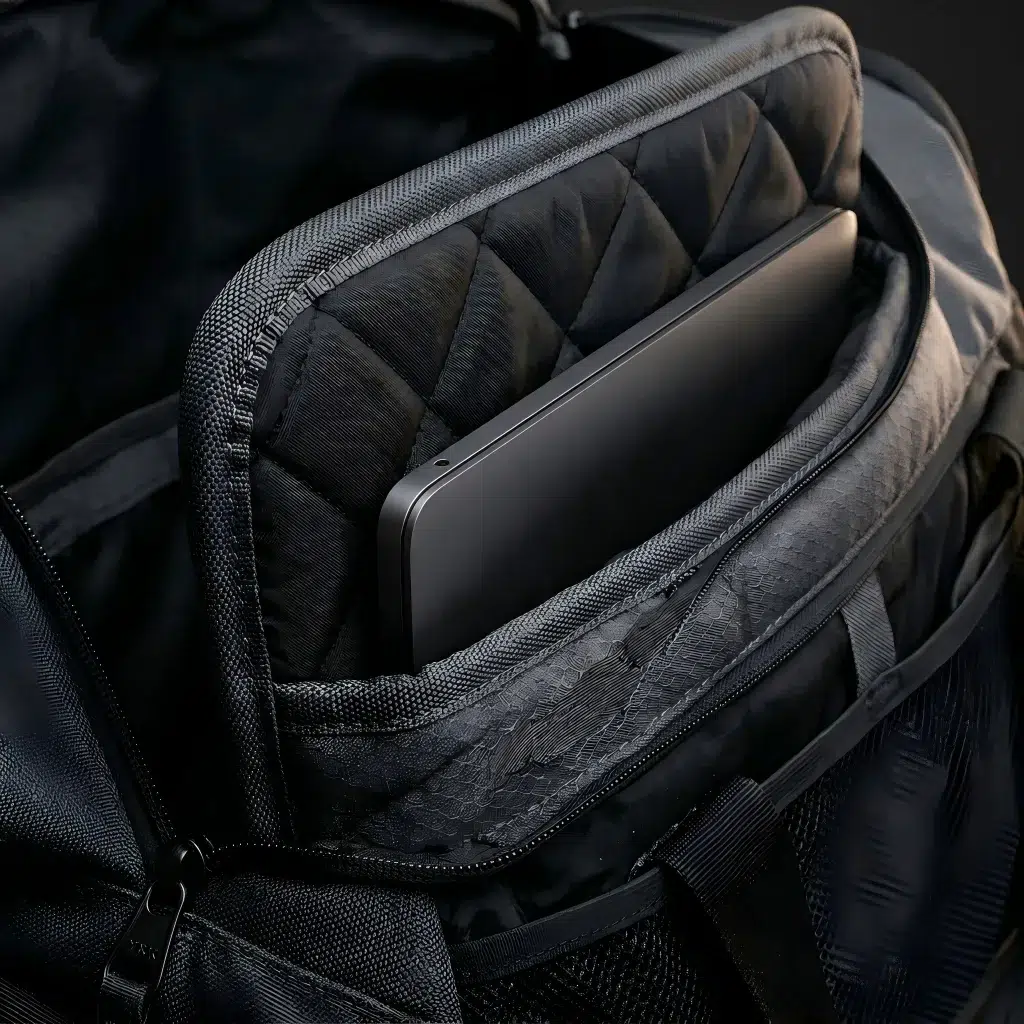
Padded 15-Inch Laptop Sleeve
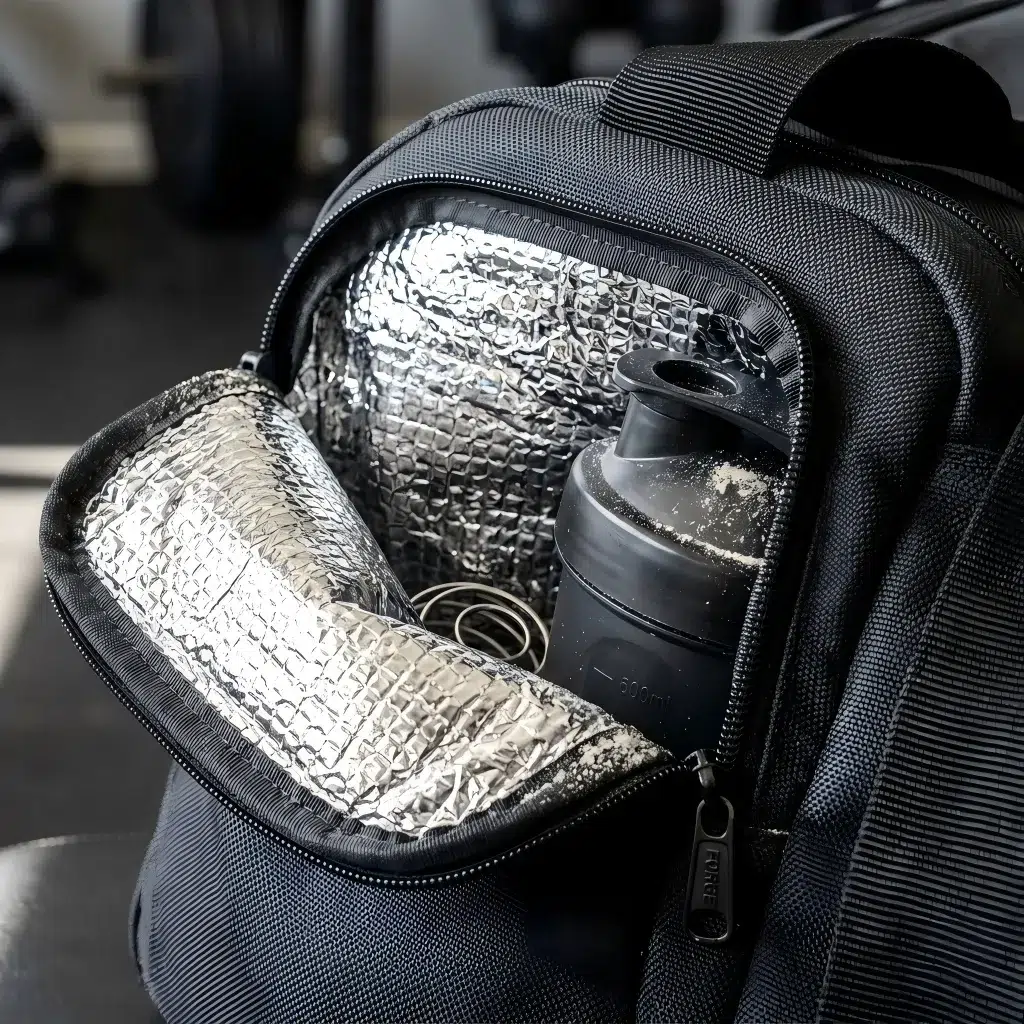
Thermal-Lined Protein Shaker Pocket

Fleece-Lined Scratch-Free Valuables Pouch
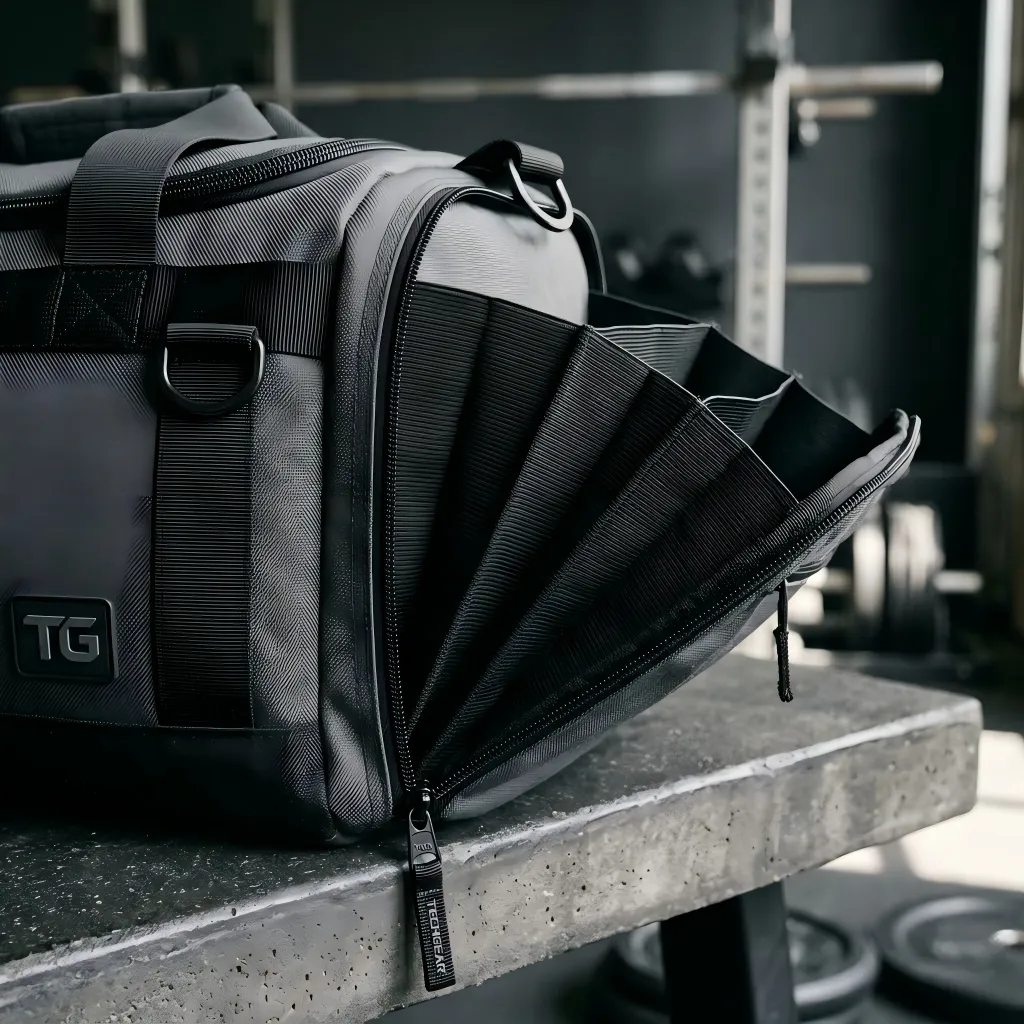
Expandable Side Storage Gussets
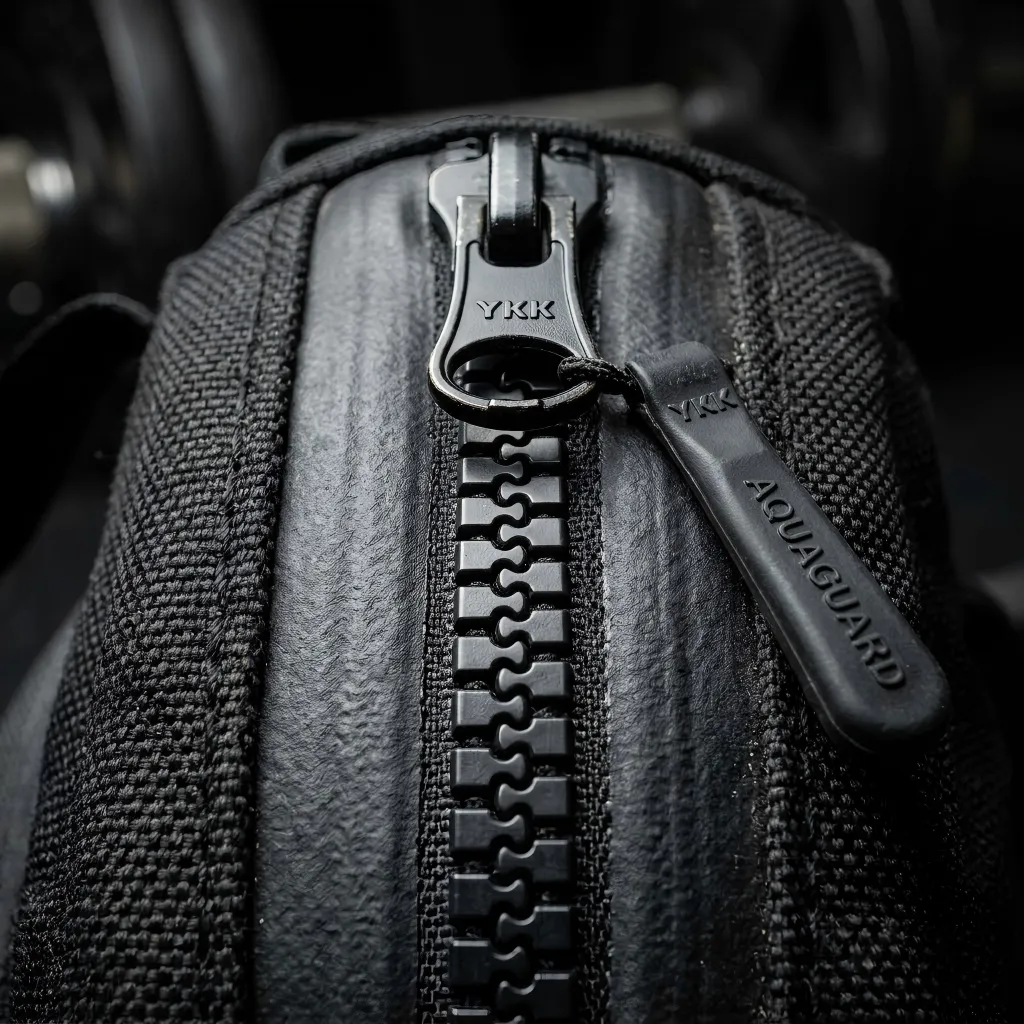
Heavy-Duty YKK Aquaguard Zippers

Matte Black Steel Hardware
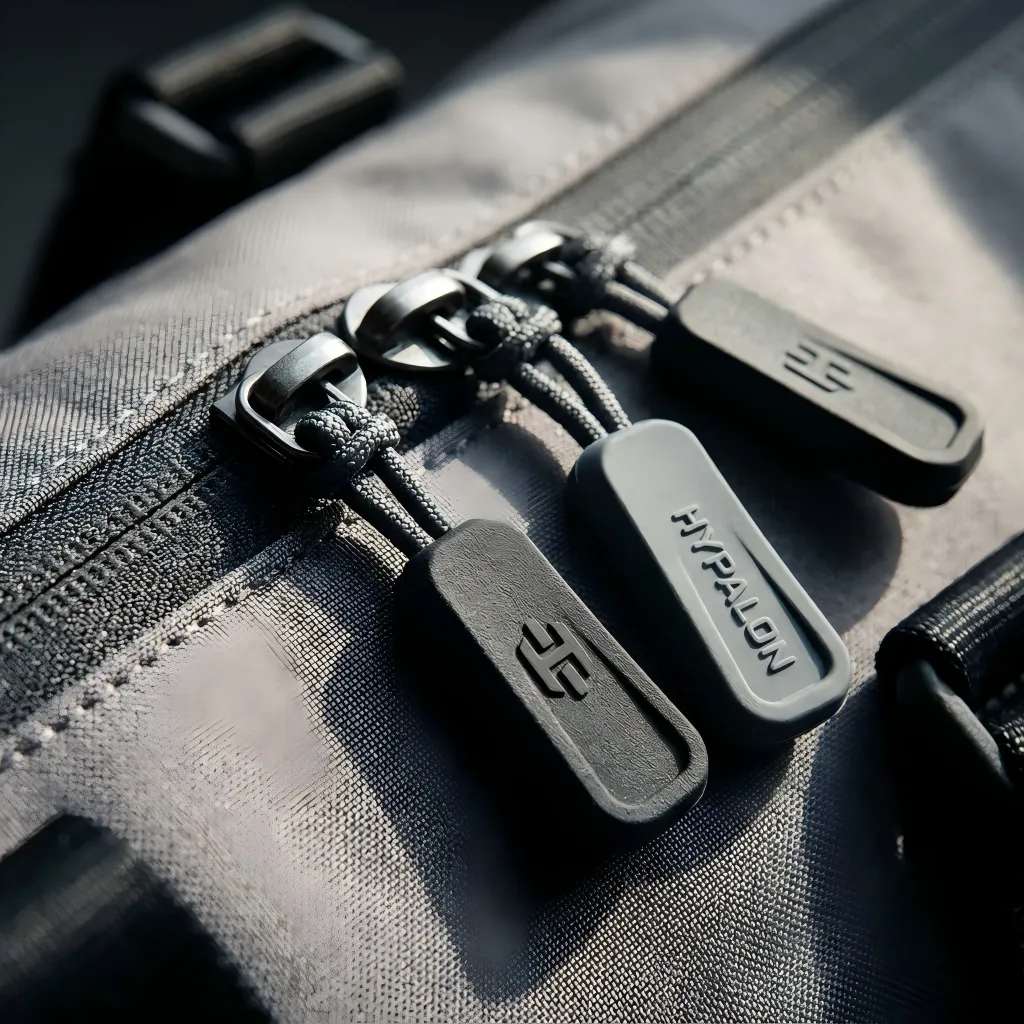
Easy-Grab Hypalon Zipper Pulls
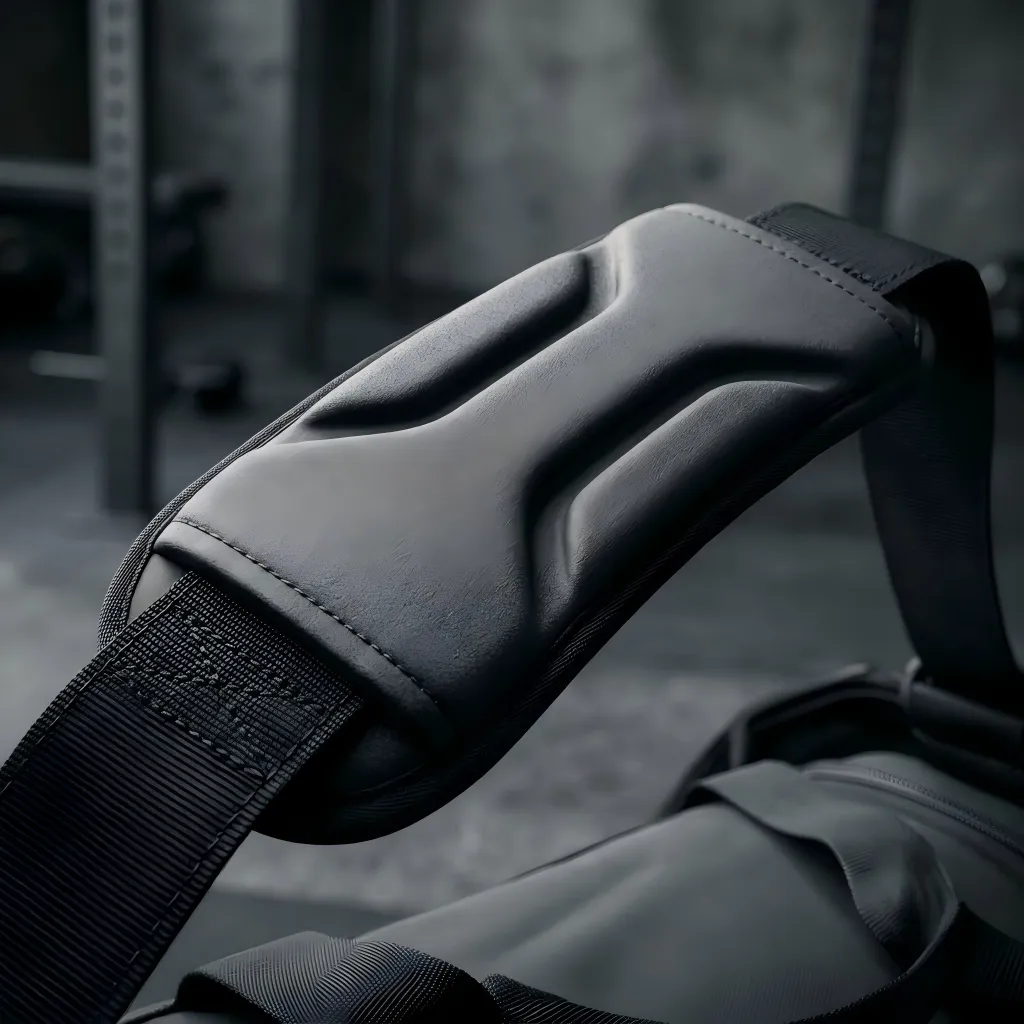
Ergonomic EVA Foam Shoulder-Pad
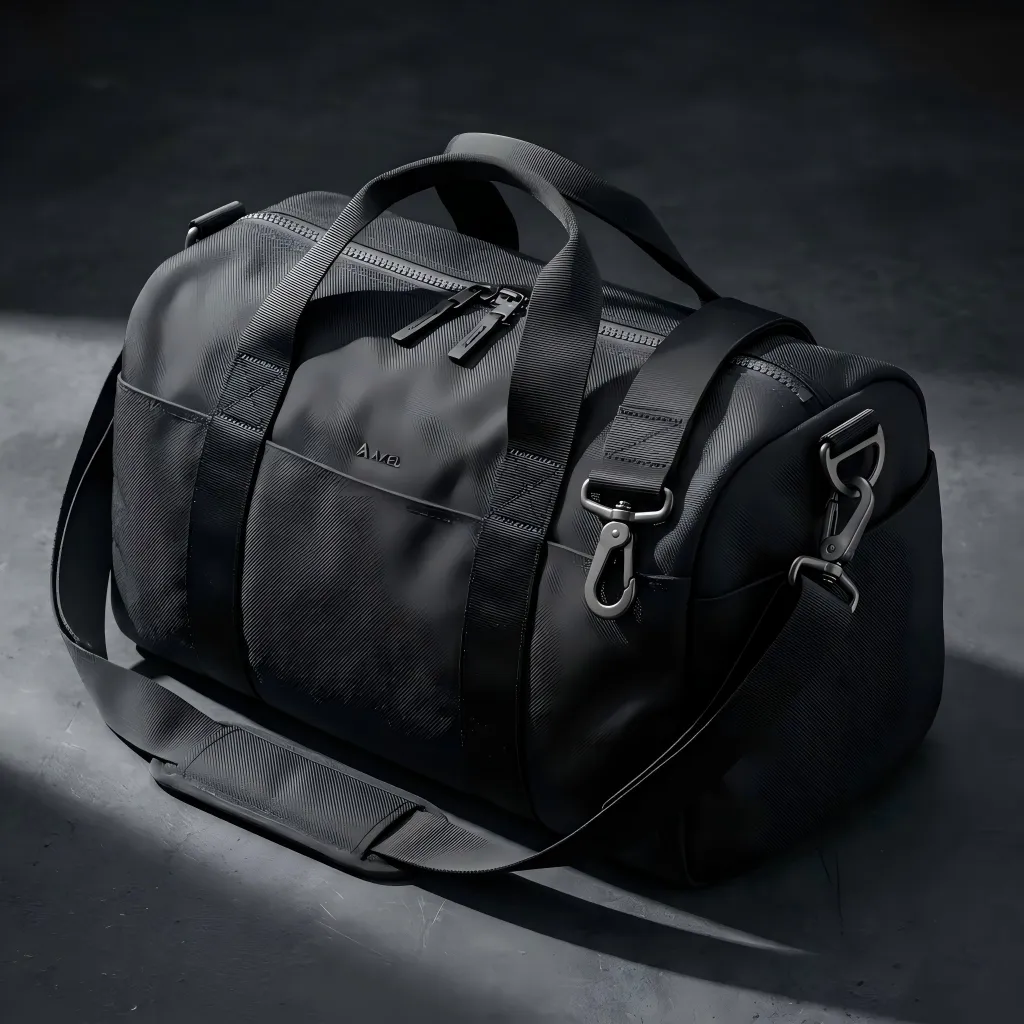
Detachable Crossbody Sling Strap
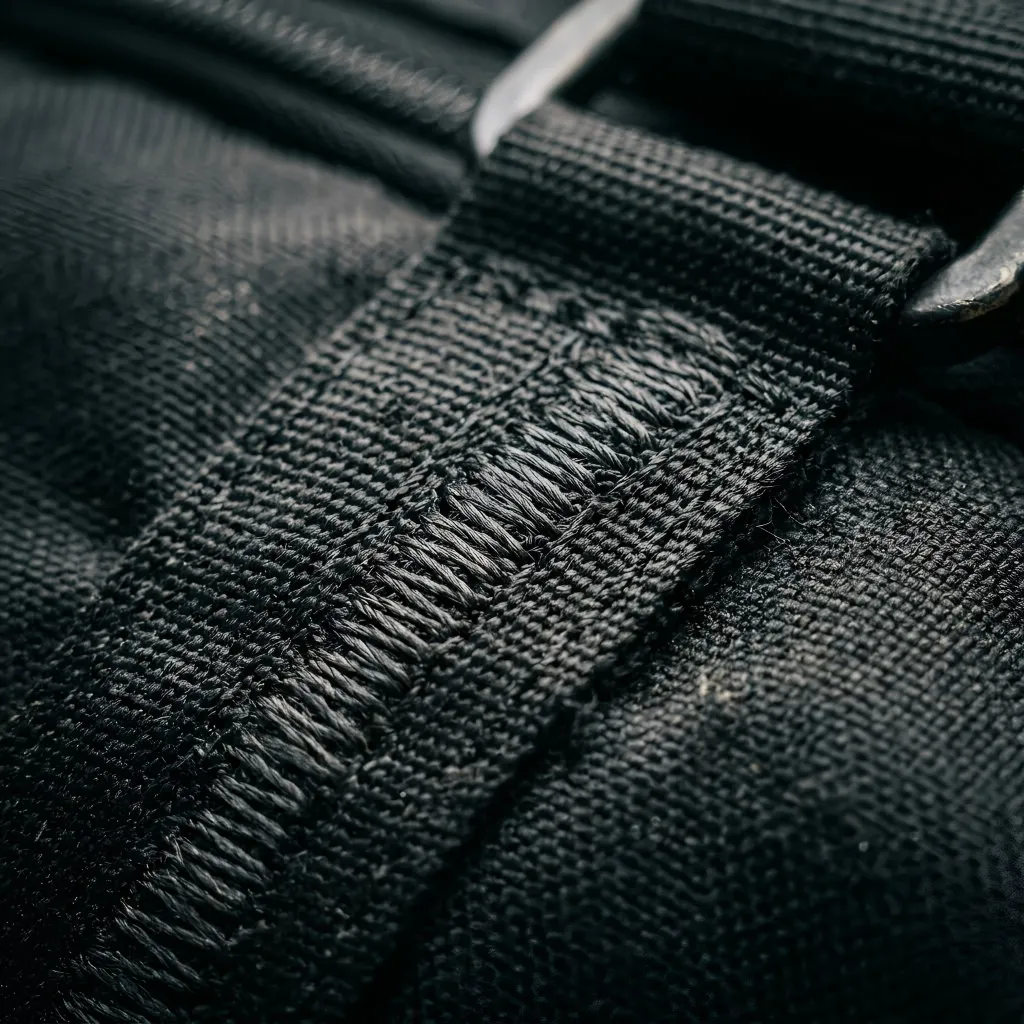
Reinforced CNC Bartack Stitching
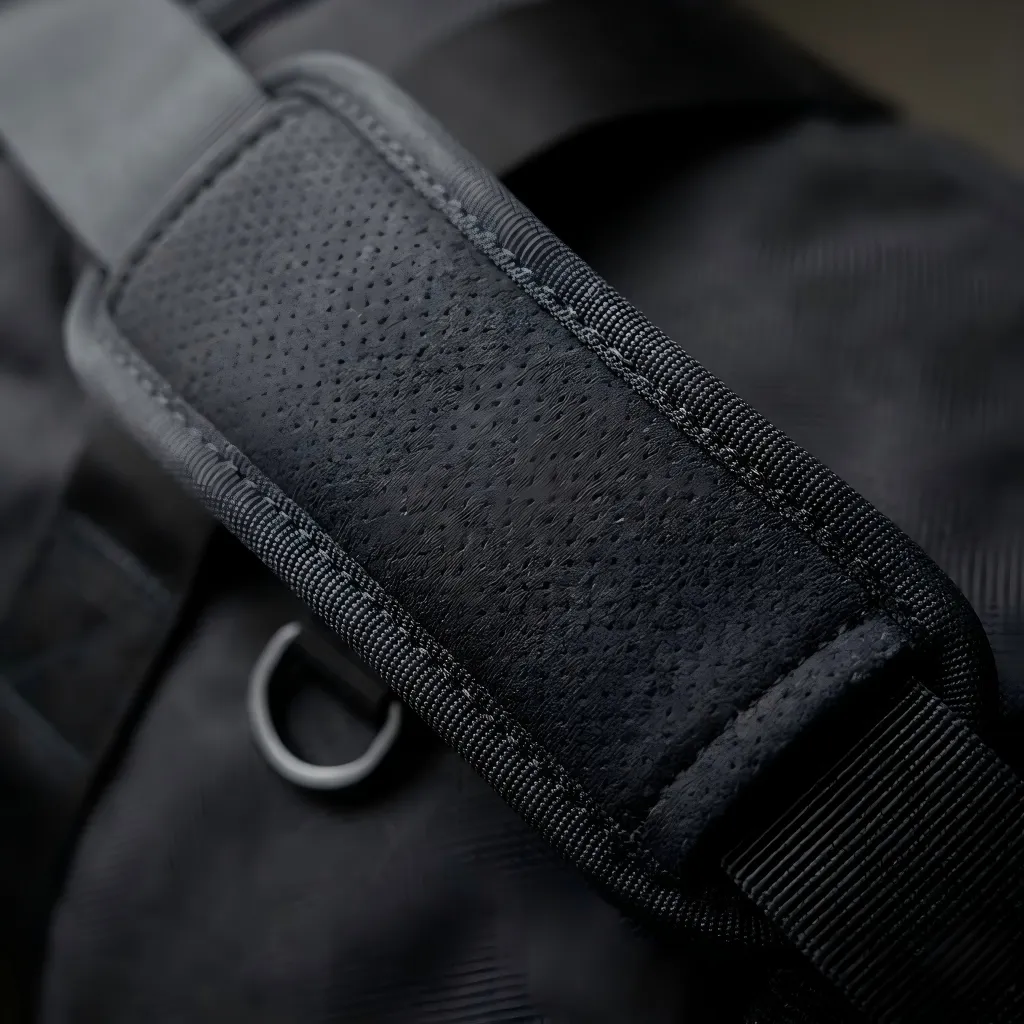
Neoprene Padded Grab Handles
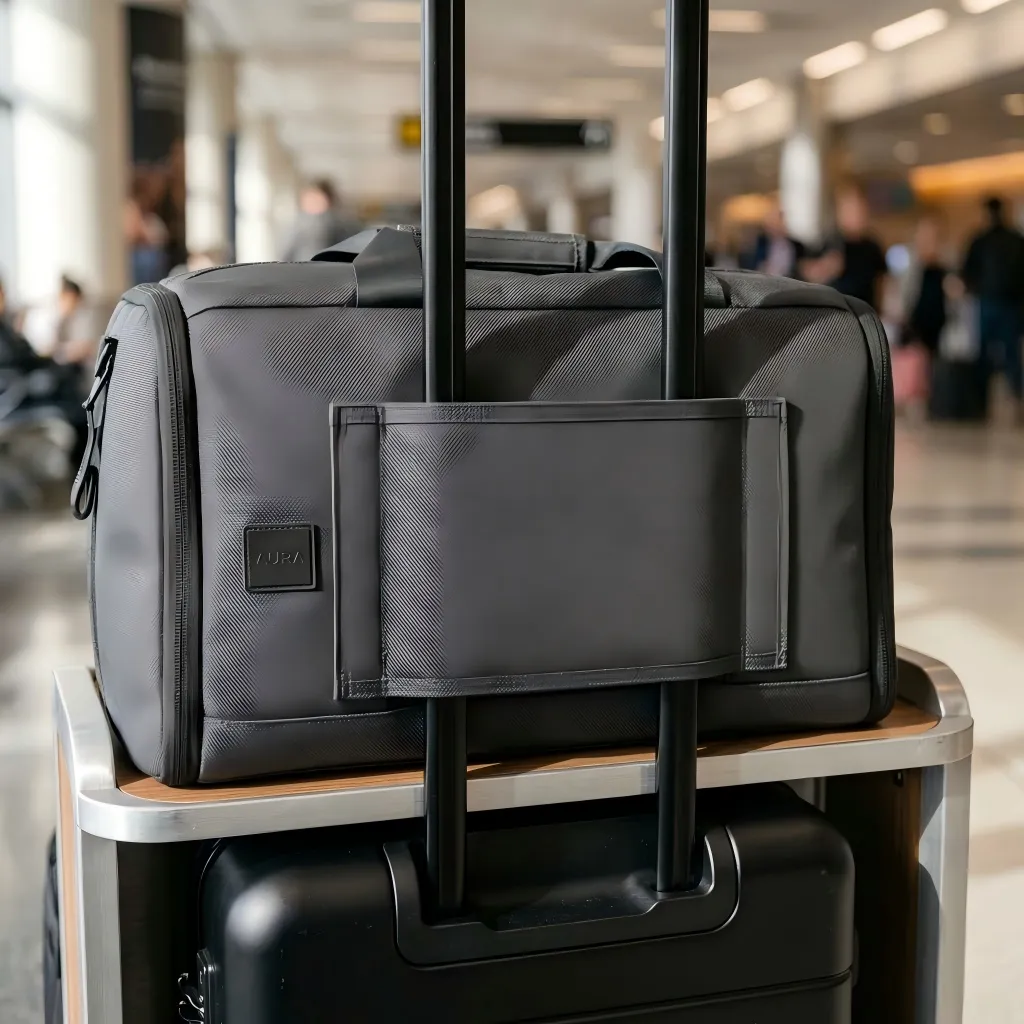
Seamless Luggage Trolley Pass-Through
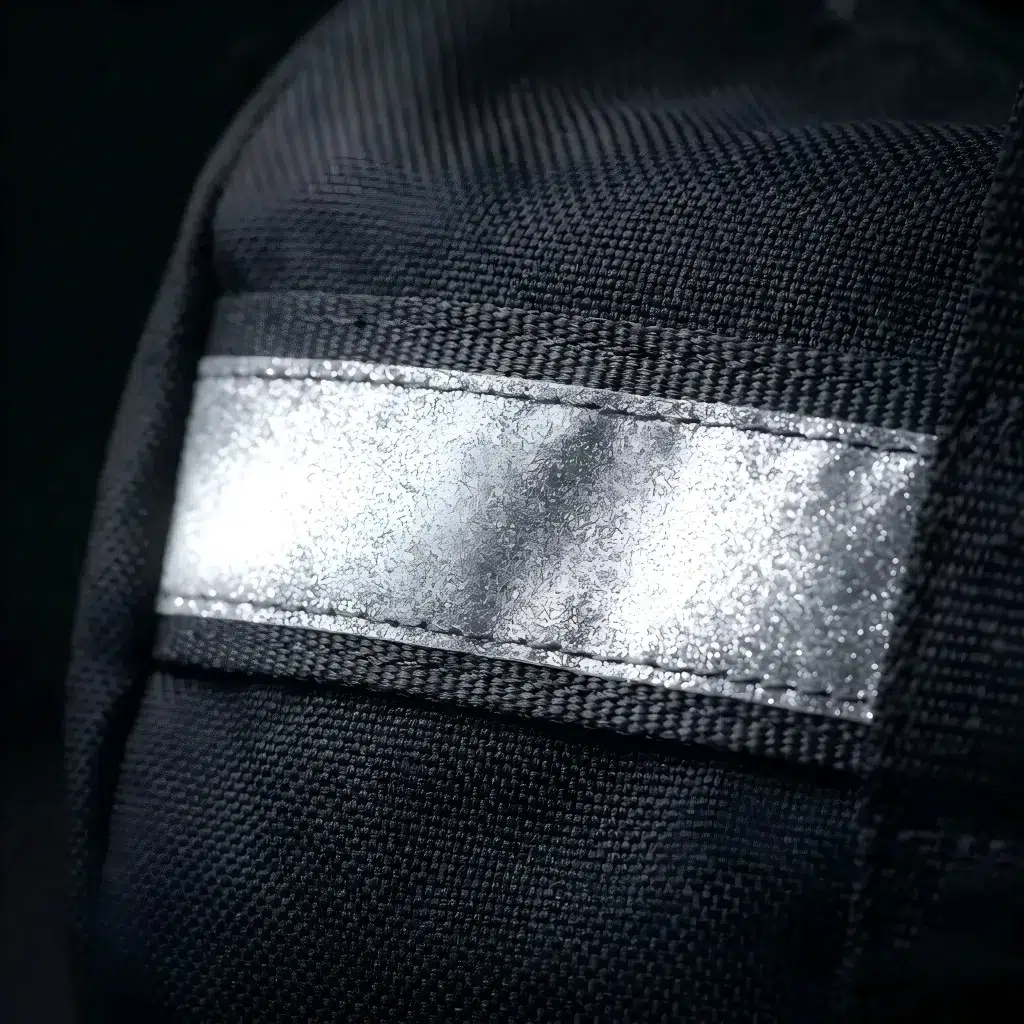
Reflective High-Visibility Safety Accents
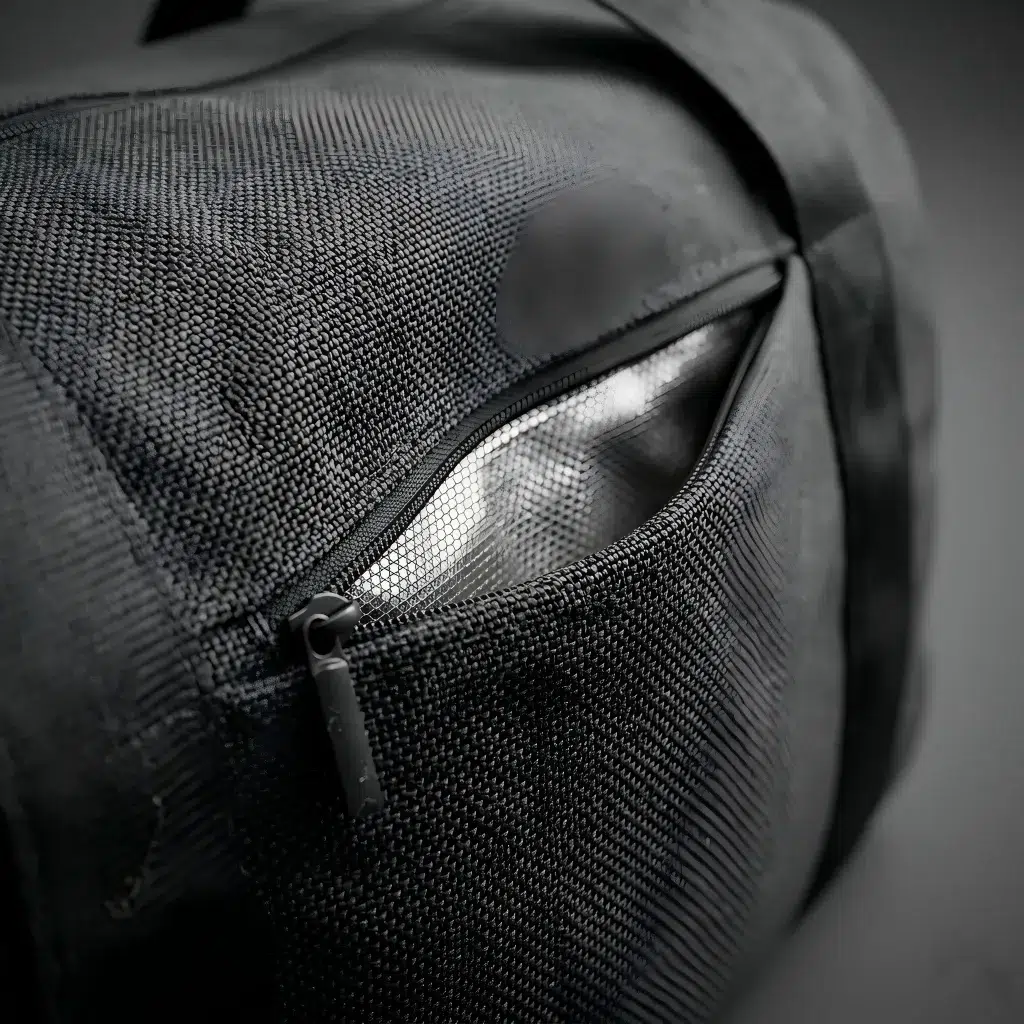
Hidden Anti-Theft RFID Pocket
Custom Gym Bag Printing Styles: A Technical Manufacturing Guide
When sourcing wholesale gym bags for your fitness brand, selecting the right customization method is just as critical as the bag’s structural design. Gym bags face harsh environments—sweat, moisture, rough locker rooms, and heavy gear.Here are the top 6 industry-standard printing methods optimized specifically for custom gym bags, ensuring your logos survive the toughest workouts:

3D High-Density Silicone Printing
- Ideal For: Premium activewear brands (e.g., Gymshark style) and modern, sporty aesthetics.
- Technical Process: Multiple layers of liquid silicone are screen-printed to create a raised, rubberized, 3D effect directly on the fabric.
- Manufacturing Logic: Medium-to-high cost. Excellent for high-end gym duffle bags.
- Expert Tip: This is the ultimate choice for fitness gear. Silicone is naturally waterproof, highly flexible, and will never crack or peel, even when the bag is stuffed full of heavy equipment.

Silk Screen Printing
- Ideal For: Solid colors and simple, bold logos.
- Technical Process: Ink is pressed through a custom mesh stencil directly onto the bag’s fabric (usually Nylon or Oxford cloth).
- Manufacturing Logic: Highly cost-effective for large bulk orders due to the initial screen setup fee. Best limited to 1-3 solid colors.
- Expert Tip: Avoid placing screen prints over seams, zippers, or the breathable mesh of a gym bag with shoe compartment, as the ink will not apply evenly.

PVC / Rubber Patches
- Ideal For: Tactical gym bags, CrossFit gear, and heavy-duty outdoor use.
- Technical Process: A 3D logo is molded from flexible PVC and securely sewn onto the bag’s exterior.
- Manufacturing Logic: Requires a one-time mold fee but offers extreme durability.
- Expert Tip: This is the superior choice for any waterproof gym bag. The patch itself is impervious to water, sweat, and UV fading, giving the bag a rugged, military-grade look.

Heat Transfer Printing
- Ideal For: Complex, multi-colored logos or photographic designs.
- Technical Process: The design is printed onto a carrier paper and thermally bonded to the bag using a commercial heat press.
- Manufacturing Logic: Excellent for smaller MOQs as it avoids high mold fees (Medium cost).
- Expert Tip: We strictly monitor heat press temperatures in our facility. Excessive heat can melt or warp lightweight synthetic nylons commonly used in packable gym bags.

Heavy-Duty Embroidery
- Ideal For: Classic branding, team sports bags, and corporate gifts.
- Technical Process: High-speed, multi-head machines stitch colored threads directly into the heavy canvas or polyester material.
- Manufacturing Logic: Priced by stitch count, not color quantity. Highly durable with a premium tactile feel.
- Expert Tip: If your gym bag has a waterproof inner lining, we recommend adding a seam-sealing tape behind the embroidery to prevent wet gym clothes from leaking moisture through the needle holes.

Sublimation Printing
- Ideal For: Edge-to-edge custom patterns (like camo) and full-bag gradients.
- Technical Process: Heat converts solid ink into a gas that permanently bonds with the fabric fibers.
- Manufacturing Logic: Zero risk of peeling or scratching off. Great for any order size.
- Expert Tip: Material Warning! Sublimation only works on light-colored, 100% Polyester fabrics. If you want a high-end Nylon gym bag, we must use a different printing method.
| Printing Method | Best For (Gym Bag Style) | Durability & Water Resistance | Cost Level | MOQ Friendliness | Key Material Restriction |
|---|---|---|---|---|---|
| 3D Silicone | Premium Activewear (Gymshark style) | High (Sweat & crack-proof) | Medium-High | Medium | Best on flat, smooth fabrics |
| Silk Screen | Bulk Promotional Gym Bags | Medium (May scratch over time) | Low (Most cost-effective) | Requires High MOQ | Works on Nylon, Oxford, Canvas |
| PVC / Rubber Patch | Tactical & CrossFit Gear | Extreme (100% Waterproof) | Medium (Requires mold fee) | Medium | Compatible with all materials |
| Heat Transfer | Multi-color / Photographic Logos | Medium (Can peel in heavy moisture) | Low-Medium | Low MOQ Friendly | Avoid thin, heat-sensitive nylons |
| Embroidery | Corporate & Team Sports Duffles | High (Very rugged) | Medium-High | Low MOQ Friendly | Needs thick fabric; requires seam sealing |
| Sublimation | Full-bag Patterns (e.g., Camo) | High (Ink bonds to fabric) | Medium | Low MOQ Friendly | 100% Light-colored Polyester ONLY |
For a waterproof gym bag, PVC rubber patches or embroidery are the best options. Heat transfer and silk screen printing can sometimes compromise the bag's waterproof coating or peel off due to moisture. Rubber patches offer 100% water resistance and a premium 3D look.
Yes, as a manufacturer, we can fully customize your order. Adding specific features like a ventilated gym bag with shoe compartment, wet/dry pockets, or custom laptop sleeves is standard practice. This requires a custom tech pack and slightly increases the manufacturing lead time.
The Minimum Order Quantity (MOQ) for a fully custom cut-and-sew gym bag typically ranges from 300 to 500 pieces per colorway. However, if you are simply adding a silk-screened logo to an existing blank inventory bag, the MOQ can be as low as 50 pieces.
Why Global Brands Trust Loomibag as Their Premier Gym Bag Manufacturer
For over 20 years, Loomibag has set the standard in athletic gear production. We engineer high-performance carriers—from a versatile sports gym bag to complex multi-functional designs—built to withstand the daily locker room grind.
Capitalizing on Q1 fitness trends requires flawless timing. Our advanced facilities utilize programmable machinery calibrated for high-volume orders. Whether you need 5,000 or 50,000 bulk gym bags, our scalable production lines guarantee on-time delivery during your peak seasons.
Athletic gear endures daily abuse. We enforce strict AQL 2.5/4.0 standards across all production lines. Every batch—including heavy-duty gym bags for men and women—undergoes dynamic load-bearing drops and 10,000-cycle zipper fatigue tests to ensure zero defects in your final shipment.
Turning a sleek sketch into functional gear requires deep expertise. Our in-house R&D team solves complex design challenges. Whether engineering a ventilated gym bag with shoe compartment or sourcing anti-microbial fabrics, we seamlessly turn your concepts into market-ready products.
Modern consumers demand safe, eco-conscious products. We ensure full compliance with REACH and California Prop 65 (phthalate and lead-free). We also offer GRS-certified RPET fabrics, allowing you to market sustainable options without regulatory friction.
Located in a premier manufacturing hub, we leverage decades-deep supplier relationships. We source premium breathable meshes and specialized zippers at highly competitive rates, optimizing costs for complex gym bags with compartments without ever sacrificing rugged quality.
Sourcing multi-functional athletic products shouldn't be a headache. Your dedicated project manager handles every nuance—from initial tech pack reviews to after-sales support—providing transparent, 24/7 communication to help your brand scale effortlessly.
The Gym Bag Manufacturer Behind Leading Fitness Brands
We bring the same elite manufacturing precision to your custom athletic gear that global sports leaders rely on every day.


Quality Assured by a Top Gym Bag Manufacturer
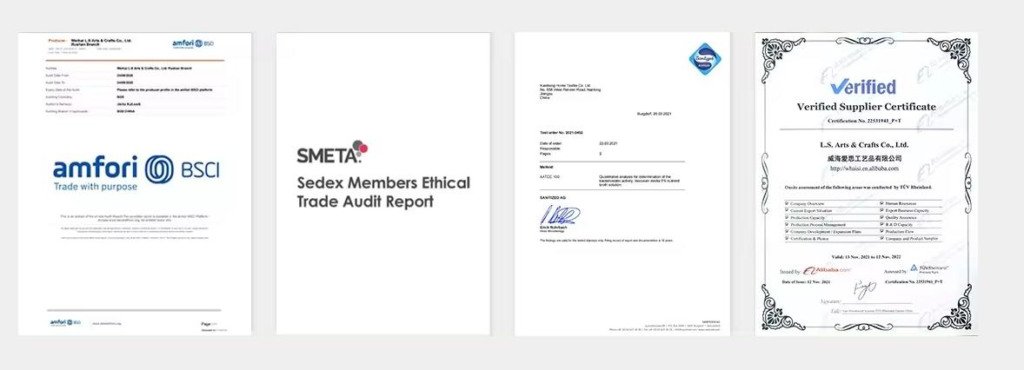
Our factory certifications reflect our commitment to excellence. We utilize audited quality control processes to deliver highly durable and premium sports bags for your brand.
- Established:2011
- Area:7500㎡,Workers:315
- Main products:All kinds of outdoor bag, funtional bag,,
- Certificate: BSCI、Sedex、SCS、C-TPAT
How Your Product is Built by a Top Gym Bag Manufacturer
We understand that fitness bags must withstand daily workouts and heavy athletic gear. As your dedicated Gym Bag Manufacturer, we implement rigorous step-by-step inspections to ensure every seam, strap, and zipper holds up perfectly from the locker room to the street.

We begin with a professional consultation to understand your exact requirements. Whether you need custom gym bags with logo placement or specific brand colors, our team gathers all manufacturing details here.

We create a physical pre-production prototype. This crucial step allows you to verify the exact gym bag dimensions, pocket layouts, and overall functionality before mass production begins.

We source premium raw materials based on your approved design. From breathable mesh to heavy-duty fabrics for a classic canvas gym bag, we prepare all necessary textiles, zippers, and hardware.

Using advanced laser and die-cut technology, we precisely cut the fabric panels. This ensures accurate shapes and consistent capacity across your entire order.

Our skilled assembly line workers stitch the panels together. We double-reinforce all shoulder straps and handles to safely support heavy athletic equipment.

We conduct strict testing on every batch. This includes heavy-load drop tests and zipper pull tests to guarantee the seams hold up under extreme pressure.

Each unit is carefully folded, protected with moisture-absorbing packets, and packed into strong export cartons. We ensure your personalized gym bags arrive in perfect retail condition.

We store the finished goods in our clean, secure warehouse. Our logistics team then helps arrange fast, reliable shipping to your requested destination.

Our support continues long after delivery. We actively collect your feedback and provide continuous service to help your fitness brand succeed.

Wholesale Gym Bags: Ready To Ship from a Top Gym Bag Manufacturer
Stock your fitness brand with confidence. From compact workout totes to heavy-duty sports duffels, our ready-to-ship inventory is built for the locker room and priced for wholesale. As a direct Gym Bag Manufacturer, we don’t just move boxes; we verify athletic performance. Every batch undergoes strict zipper pull and load-bearing tests before leaving our facility, ensuring you receive durable, defect-free gear that athletes can trust—shipped immediately.

Precision-Crafted Gym Bags: Direct From A Certified Gym Bag Manufacturer
When sourcing inventory, your biggest risk is expensive customer returns caused by blown zippers, torn straps, or failing compartments. As a specialized Gym Bag Manufacturer, we engineer our bags to survive overstuffed lockers, wet towels, and heavy daily use. We eliminate your quality control headaches before the shipment ever leaves our factory floor.
● 01.Odor Control & Compartment Integrity
How do you ensure the lining in a gym bag with shoe compartment won't tear or trap foul odors after repeated use?
We construct the inner dividers using 210D anti-microbial ripstop polyester, reinforced with double-needle stitching. To prevent odor buildup, we integrate laser-cut ventilation eyelets that allow active airflow while keeping the main compartment completely isolated from dirty shoes.
What testing verifies that wet towels won't leak into the dry zones?
We use a 100% TPU-lined interior for the wet pockets, sealed with high-frequency welding rather than standard needle stitching. Every batch is subjected to a 24-hour moisture barrier test to guarantee zero water transfer into the dry areas.
● 02. Load-Bearing & Suspension
How do you test the shoulder strap attachment points for a heavy duty gym bag meant to carry lifting belts and weights?
Every stress point is reinforced with computer-controlled Bar-Tack stitching using industrial nylon thread. We test these points on an ISO-certified tensile machine, ensuring they withstand a continuous 30kg (66 lbs) drop-jerk force without thread failure.
What prevents the base of the bag from wearing out on rough locker room tiles?
We build the base panel using abrasion-resistant 900D ballistic nylon coated with a thick Polyurethane (PU) layer. We also install high-density rubberized bottom feet to elevate the fabric away from friction and wet floors.
● 03. Material Performance & Weather Resistance
What outer shell materials do you use to manufacture a truly waterproof gym bag that won't crack in cold weather?
We use a high-density 600D Oxford polyester treated with a deep-penetrating DWR (Durable Water Repellent) coating. The fabric undergoes cold-flex testing at -15°C (5°F) to ensure the coating remains flexible and will not peel or crack over time.
How do you prevent zipper track blowouts when users overstuff their gym duffle bag?
We exclusively use SBS or YKK heavy-duty coil zippers (size #8 or #10). During our factory QC process, these zippers are put on a reciprocating test machine for 5,000 cycles under lateral tension to guarantee the teeth will not separate when the bag is packed to maximum capacity.
● 04. Branding & Finish Quality
When producing custom gym bags with logo, how do you guarantee the print won't peel or fade from sweat and friction?
For printed logos, we use eco-friendly plastisol inks cured through a high-temperature tunnel dryer at 160°C. We then perform an ISO 105-X12 colorfastness test to rubbing and perspiration, ensuring your branding remains permanent and vibrant.
How does your factory verify that the fabric dyes won't bleed onto a user's light-colored clothing?
We source fabrics strictly from mills that pass ISO 105-E04 colorfastness tests. This ensures the dyes remain permanently locked into the fibers, guaranteeing zero color transfer onto the user’s skin or expensive workout gear.
Partner with a leading Gym Bag Manufacturer. We provide full OEM/ODM customization, heavy-duty materials, and strict QC—delivering defect-free products directly from our factory to your warehouse.
Your customers push their limits; their gear should too. Stop losing sales to split seams and broken zippers. From ventilated duffels to heavy-duty CrossFit bags, we deliver the gym-tested reliability active lifestyles demand. Equip your brand for growth.
- Sweat & Tear Resistant: Built for the locker room and the gym floor. Premium materials mean happier customers and fewer returns eating into your profit.
- Factory-Direct Margins: Cut out the trading companies. Partner directly with a leading Gym Bag Manufacturer to access Tier-1 pricing and maximize your ROI.
- Agile OEM/ODM Supply: Whether you need custom branding (like shoe compartments or wet pockets) or a quick restock of best-sellers, our production lines are ready to scale
 English
 Turkish
 German
 Dutch
 French
 Danish
 Finnish
 Swedish
 Italian
 Polish
 Portuguese
 Spanish